TL;DR

Get tools and workshop supplies delivered free — and shop member deals
- Fast, free delivery on millions of items
- Access to Prime Big Deal Days deals on October 6–7
- Prime Video, Amazon Music and more included
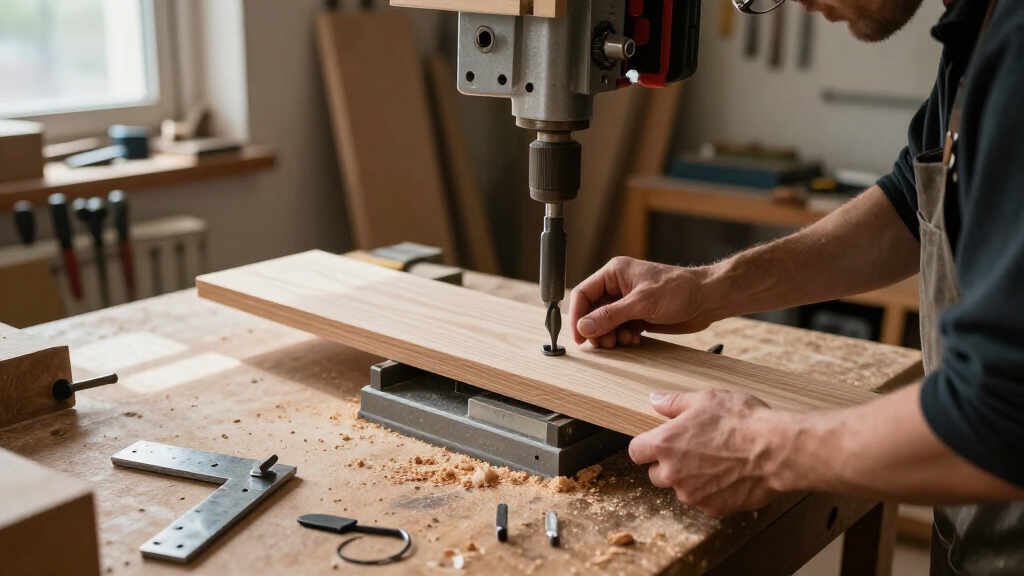
A drill press makes perpendicular, repeatable holes easier than a handheld drill, but accuracy depends on the chuck, spindle, table, bit and workholding being set up correctly. Unplug the machine before adjustments, measure runout with a dial indicator when possible, square the table in two directions, and confirm each setup with a test hole in scrap.
A drill press can bore a clean row of perpendicular holes, then ruin the next board because the table slipped a hair when you locked it. The machine looks steady; the cut tells a different story. A few simple checks can help you tell whether the problem comes from the setup, the bit or a worn part.
This guide walks you through safe calibration with practical shop tools: checking spindle and chuck runout, squaring the table, setting depth, choosing speed and holding work securely. You’ll also learn what a test hole can reveal before you commit to a finished cabinet panel or a row of dowel holes.
You don’t need a metrology lab to improve a home-shop drill press. A machinist’s square, straight test rod, scrap stock and a dial indicator where available will catch many common problems. The aim is useful accuracy for the job in front of you, not chasing a universal tolerance that may not fit your machine or your work.
Unplug the press before adjusting the chuck, belt, table or depth stop; clamp work and remove the chuck key before startup.
Use a dial indicator and straight test rod to separate spindle or chuck runout from a bent or poorly clamped bit.
Square the table front-to-back and side-to-side, then recheck after locking it because the clamp can shift the angle.
Use a depth stop for hole depth and a fence or stop block for hole location; neither replaces secure workholding.
Pick speed from the machine and bit makers’ guidance, then confirm the setup with a test hole in matching scrap.
Tips for Calibration and Fine-Tuning Your Drill Press
A drill press makes perpendicular, repeatable holes easier. Accuracy comes from the whole setup: chuck, spindle, table, bit and workholding. Check alignment, adjust safely and prove the result on scrap before drilling a finished part.
Make the setup stable and safe
Calibration starts with a planted machine and a safe work area. Leveling helps stability, but it does not prove that the spindle is square to the table.
Unplug before adjustments
Disconnect power before handling the chuck, belt, table or depth stop. Follow the manual for belt tension, lubrication and permitted service.
Stop wobble at the source
Secure the press to a stable bench or stand. Firm the base and fasteners; a flexing bench can undermine careful setup.
Secure the work
Clamp the workpiece, remove the chuck key, wear eye protection and keep hair, gloves and loose sleeves clear of rotating parts.
Check runout before blaming the chuck
Runout is the side-to-side movement of the spindle, chuck or bit as it turns. It can widen holes, roughen edges or move a hole off center.
- With power disconnected, mount a dial indicator securely against the spindle or a known-straight test rod.
- Turn the spindle by hand and watch the reading. A changing reading shows movement; it does not identify the faulty part by itself.
- Clean dust, pitch and nicks from the taper surfaces, then reseat the chuck as the manufacturer directs.
- If a rod runs true but a bit wobbles, inspect the bit and how it sits in the jaws. If both wobble, check chuck seating and spindle assembly.
Square the table in two directions
Use a machinist’s square beside a straight test rod, or another suitable square-and-rod method. Adjust the tilt, lock the table and recheck both axes.
Check the whole stack: bit, table, stock
A table leaning left can steer a hole toward the face of a shelf. Square the setup, hold the shelf against a fence, and drill a test hole in scrap of matching thickness. A bowed board or tilted vise can still change the result.
Depth and location are separate settings
A depth stop limits spindle travel. A fence or stop block sets where the hole lands. Repeatable work often needs both, plus secure clamping.
Set the depth stop
Unplug the press, lower the spindle to the target, set the stop according to the manual and test the exact bit and stock on scrap.
Add a fence or stop block
Use a fence to align the edge and a stop block to repeat the starting position across pieces, such as shelf-pin panels.
Clamp against movement
Clamp the work against the fence and block. If a bit catches, an unclamped panel can shift, spoil spacing or cause injury.
Choose a sensible speed, then test
Use the machine and bit makers’ guidance as your starting point. Material, bit type and operation all matter, so there is no universal speed for every job.
Match speed to bit and material
Larger bits and harder materials generally call for slower spindle speeds. Smaller bits and softer materials can use faster speeds. Change belt positions only with power disconnected and follow the manual.
Steady pressure; clean surfaces
Use steady pressure suited to the bit and material. Too much force can overheat or damage a bit; too little can make it rub. Keep tapers and the table clean, and inspect belts, pulleys, fasteners and chuck for wear.
Change one thing at a time
Prove the setup on matching scrap before committing to a cabinet panel, hinge cup or row of dowel holes. Check location, angle and finish.
Stabilize
Anchor the press and clear loose work.
Measure
Check runout with a straight rod and indicator if available.
Square
Align both directions, lock and recheck.
Set
Choose speed, depth and position; clamp the stock.
Verify
Drill scrap and inspect the hole before final work.
Make the press stable and safe before you adjust it
Start calibration with the press unplugged, stable and free of loose work. That gives you a safe way to handle the chuck, belt, table and depth stop while you check what moves. Clamp the machine securely to a bench or floor stand, remove any wobble from the base, and check that the head and column fasteners feel firm.
A level machine helps it sit steadily, but a level base does not prove that the spindle points square to the table. Think of leveling as keeping the tool planted; squaring is a separate alignment check. In a small garage shop, a press on a bench that flexes when you lean on it can make accurate setup feel impossible, so fix the bench or anchor the machine before blaming the spindle.
Before turning the press on, remove the chuck key and clamp the workpiece. Wear eye protection, tie back long hair and keep gloves and loose sleeves away from rotating parts. If you’re drilling a small brass plate, a vise or clamp prevents the plate from spinning like a propeller when the bit grabs.
Make adjustments only with power disconnected. Follow the manual for belt tension, lubrication and permitted service. A cracked pulley, persistent spindle play or unusual grinding noise calls for proper repair, not a more forceful adjustment at the table.
As an affiliate, we earn on qualifying purchases.
Measure runout before you blame the chuck
Runout is the side-to-side movement you see when the spindle, chuck or bit rotates. Too much can widen a hole, leave a rough edge or shift its center. A dial indicator is the clearest way to measure that movement: with the press unplugged, mount it securely against the spindle or a known-straight test rod, then turn the spindle by hand and watch the reading.
If the needle swings, check simple causes before replacing parts. Dust, pitch or a nick on the arbor and chuck tapers can keep the chuck from seating cleanly. A bent rod or a drill bit held off-center can also look like spindle trouble. Clean the mating surfaces carefully and reseat the chuck as the manufacturer directs.
Try this example: a fresh bit appears to wobble while you’re drilling a hinge cup in a cabinet door. Swap it for a straight test rod and rotate the spindle by hand. If the rod runs true but the bit wobbles, inspect the bit and how it sits in the jaws; if both wobble, look at the chuck seating and spindle assembly.
Without an indicator, you can still look for obvious movement, but don’t mistake that visual check for a precise measurement. If runout stays excessive after cleaning and reseating, or the spindle has play, stop and seek qualified service. A bent spindle is a repair problem, not a table calibration problem.
As an affiliate, we earn on qualifying purchases.
Square the table so holes meet the work at 90 degrees
To make perpendicular holes easier than with a handheld drill, square the table to the spindle in two directions: front-to-back and side-to-side. Use a machinist’s square beside a straight test rod in the chuck, or another suitable square-and-rod method. Adjust the table tilt, lock it, and check both directions again.
The lock deserves a second look. On some presses, tightening the table clamp nudges the angle just enough to spoil the setting. A table’s printed angle scale is useful for rough positioning, but it is not a precision reference; verify a required angle with an appropriate gauge instead of trusting the pointer.
Suppose you’re drilling dowel holes in the edge of a shelf. A table that leans left may make the bit wander toward the face, so the joint closes poorly even though the holes look centered from above. Square the setup, clamp the shelf flat against a fence, and drill a test hole in scrap of matching thickness before cutting the real part.
Think of a square table as the reference surface for the work, not a promise that every hole will be perfect. A bowed board, a tilted vise or a workpiece that isn’t flat can still change the result. Check the whole setup from bit to table to stock, then test the hole that matters.
As an affiliate, we earn on qualifying purchases.
Set depth and location separately for repeatable holes
A depth stop controls how far the spindle travels; a fence or stop block controls where the hole lands. They solve different problems, and repeatable drilling usually needs both. With the press unplugged, lower the spindle to the desired depth, set the stop according to the manual, and drill a test hole in scrap. The distinction matters because a perfect depth setting cannot correct a hole placed too close to an edge, and a fence cannot keep a deep bit from breaking through the back.
For a row of shelf-pin holes, a stop block gives each workpiece the same starting position while a fence keeps its edge aligned. Clamp the panel against both. The depth stop can then keep each hole from breaking through the back, but it cannot prevent the panel from sliding sideways if you leave it loose. Secure workholding is part of accuracy as well as safety: if the bit catches, an unclamped panel can shift and ruin the spacing or cause injury.
On a thick board, remember that a depth setting at the spindle may not equal the final hole depth if you change bits or add a backing board. The tip geometry affects where the hole begins and ends, and the board or support changes how far the bit can travel before reaching the underside. Test the exact bit, stock thickness and support you’ll use for the finished work. A scrap test is cheap; patching a row of accidental through-holes in a cabinet side is not.
For blind holes, mark the target depth clearly and inspect the test piece from both faces where practical. A shallower hole preserves more material and lowers the chance of breaking through, but may leave too little room for a fastener or glue. If the stop feels inconsistent, check for loose hardware or sticking travel before relying on it. Make one adjustment at a time, then verify with the same setup and material.
As an affiliate, we earn on qualifying purchases.
Choose a speed that suits the bit and material
Choose spindle speed from the machine’s chart and the bit maker’s guidance, then treat that setting as a starting point. Larger bits and harder materials generally call for slower speeds; smaller bits and softer materials can usually run faster. There is no single speed that fits every material, bit geometry and operation.
For example, a large Forstner bit boring a flat-bottomed hole in hardwood needs a different approach from a small twist bit piercing pine. If the cut smells scorched or the bit heats quickly, stop and reassess speed, sharpness and feed. In metal, a dull bit and excessive speed can turn a neat hole into a squealing, hot mess.
Change belt positions only with the machine unplugged, and use the manual’s belt-tension instructions. During drilling, apply steady pressure suited to the bit. Too much force can overheat or damage the cutting edge; too little can make the tool rub instead of cut. Listen to the sound and watch the chips, but don’t use noise alone as a speed gauge.
When the press has no readable chart, look up the machine and bit makers’ recommendations rather than borrowing a number from an unrelated setup. Online calculators can help estimate a starting speed, but confirm that the advice matches the material and tool. Test on scrap and adjust based on clean cutting, chip shape and heat.
Use a repeatable tune-up sequence and prove it on scrap
A useful tune-up makes one change at a time and checks the result on the work you actually plan to drill. Calibration is not a magic number; it is a setup you can repeat. Run this sequence when a hole looks angled, oversized or rough, or after moving the table or changing the chuck.
- Unplug the press, secure the base and inspect the chuck, belt, pulleys and fasteners for visible damage or looseness.
- Check the bit and runout with a known-straight rod or dial indicator; clean and reseat taper surfaces if needed.
- Square and lock the table in both directions, then recheck the angle after tightening.
- Set stops and workholding for the job: depth stop for travel, fence or stop block for location, clamps for the stock.
- Select a suitable speed from the machine and bit guidance, then make a test hole in matching scrap.
Imagine you’re boring a dozen holes for a small stool. A single test hole in the same hardwood lets you check the entry, exit, angle and depth before the first leg is spoiled. Mark the setup or write down the speed and stop positions if you’ll need to repeat it next week.
Keep chips clear enough to see your layout marks and keep the bit from packing with debris. Use suitable dust extraction or chip control for the material and operation, while keeping hoses and hands away from the rotating tool. After the test, inspect the hole and change only the part of the setup that explains the defect.
Know when a rough hole points to maintenance or repair
A rough or oversized hole can come from several small causes: runout, a dull or bent bit, poor chuck grip, moving stock, unsuitable speed or excessive feed. In wood, tear-out also depends on the bit, backing support and drilling technique. Check these factors before deciding the press itself has failed.
If a hole is ragged only as the bit exits a thin board, add a sacrificial backing board and clamp the work. If the hole starts in the wrong place, improve the fence or workpiece layout. If every bit visibly wobbles, test with a straight rod and inspect the chuck seating before buying a replacement chuck.
Routine care is simple: keep the table, spindle area and taper surfaces clean; inspect belts and pulleys for wear; check fasteners; and lubricate only where the maker specifies. A dusty press in a garage can collect fine wood dust around the table and motor, so clear it regularly without brushing near live or moving parts.
Persistent spindle play, unusual noise, damaged parts or runout that remains high after basic checks are signs to stop and get service. Don’t disassemble components beyond the manufacturer’s instructions. The right calibration is useful; forcing a damaged assembly back into alignment can make the repair worse.
Frequently Asked Questions
How can I tell if my drill press is out of alignment?
Look for recurring angled holes, visible wobble, inconsistent results or a table that shifts when you lock it. Check runout with a dial indicator or known-straight test rod, then check table squareness front-to-back and side-to-side.
Why does the bit wobble in the chuck?
The bit may be bent or poorly clamped, or the chuck may not be seated cleanly on its taper. Test with a known-straight rod and inspect the taper surfaces before deciding the spindle or chuck needs repair.
How accurate should a drill press be?
Useful accuracy depends on the job and the machine; a universal tolerance would be misleading. Measure runout and squareness, then judge whether the results meet the needs of your work, such as a loose clearance hole or a tight dowel joint.
What speed should I use for drilling?
Use the drill press chart and bit maker’s recommendations as your starting point. Larger bits and harder materials generally need slower speeds, while bit type and operation can change the choice; confirm it on scrap.
Can I adjust the table or belt while the press is running?
No. Unplug the press before adjusting the table, belt, chuck, spindle setup or depth stop. Clamp the workpiece and remove the chuck key before powering up.
When should I have the drill press serviced?
Get service if the spindle has persistent play, the machine makes unusual noises, parts look damaged or excessive runout remains after cleaning and reseating components. Follow the manufacturer’s repair instructions and don’t force an adjustment that does not correct the problem.
Conclusion
Remember this: a drill press is only as accurate as the setup you can verify. Check runout, square the table in both directions, clamp the work and test depth and speed on scrap before you touch the finished piece.
Make one adjustment at a time, and let the test hole tell you what to fix. A clean, square hole should leave a crisp edge and a quiet machine; that’s a better shop signal than any angle printed on a table scale.
Halloween Picks
halloween
As an affiliate, we earn on qualifying purchases.