TL;DR
Open a free Amazon Business account
Business pricing, bulk buying and tax-exempt orders.
Create a free accountAs an affiliate, we earn on qualifying purchases.
An efficient dust collection system is designed from the pickup hood to the exhaust, not simply by connecting machines to a large fan. Size each duct section for its actual airflow, use short smooth routes, limit flexible hose, and verify performance under realistic operating conditions rather than trusting a free-air CFM label.
A dust collector can roar like a small aircraft and still leave a pale blanket of powder across your table saw. The problem often hides above your head: too much flexible hose, sharp branch entries, an oversized main, or a maze of elbows quietly consuming the airflow promised on the collector label.
You will get better results when you treat collection as a complete airflow path. That path starts where the cutter throws debris, passes through the pickup hood, ductwork, separator, and filter, and ends at the fan exhaust. Every fitting takes a small bite out of the available pressure, and those bites add up fast.
This guide shows you how to size branches, route a main, choose fittings, manage gates, and check the finished system with real measurements. You will also see where the usual rules have limits, especially when combustible wood dust, indoor air return, electrical work, or several machines running together enter the plan. The goal is practical: more dust disappearing with a clean whoosh, less powder hanging in the light, and fewer chips waiting inside your ductwork.
Calculate duct diameter from required pickup CFM and conveying velocity; do not copy the collector inlet size across every branch.
Use rigid round duct, shallow-angle wyes, long-radius elbows, and only short flexible connections to protect the fan’s available pressure.
Evaluate the hardest active route with realistic filter loading, then check combined airflow whenever several machines can operate together.
Record airflow and pressure baselines after commissioning, and investigate recurring deposits as an operating or design fault.
Treat combustible-dust protection, electrical work, and indoor air return as safety and code matters that may require qualified professionals.
Maximizing Dust Collection Efficiency with Piping Layouts
A collector can roar while dust still settles across the shop. The real system begins at the pickup hood, continues through every duct and fitting, and ends at the exhaust. Design the entire airflow path—not merely the fan connection.
Get both air speeds right.
Transport speed inside a duct cannot recover dust that has already escaped the hood. Watch the debris stream first, position the opening close to its source, and then size the branch to carry the captured material.
Capture airflow
Pulls dust into the hood before the cutter, belt, or blade throws it into the room. Hood shape, distance, orientation, and process energy determine how much air is required.
Conveying velocity
Keeps captured particles moving through horizontal runs, risers, fittings, and the separator. Material size, density, moisture, and shape influence the required speed.
More area requires more air.
The same 400 CFM behaves very differently in 4-inch and 6-inch round ducts. The wider duct has 2.25 times the cross-sectional area, so velocity falls sharply unless the fan supplies additional volume.
Velocity at 400 CFM
Illustrative average velocities for round duct. Final sizing must reflect actual hood demand, material, resistance, fan performance, and applicable standards.
Match the pipe to its real load.
Branches serve individual pickups. Mains normally grow after airflows merge. A single diameter throughout the shop ignores simultaneous use, resistance, and the changing volume carried by each section.
| Layout Choice | Airflow Effect | Visible Warning | Better Response |
|---|---|---|---|
| Duct Too Large | Velocity drops at the available CFM. | Chips collect along horizontal runs and low spots. | Match diameter to pickup airflow and transport speed. |
| Duct Too Small | Friction and static-pressure loss rise. | Sharp hiss, weak distant pickup, and heavy restriction. | Enlarge only where supported by sufficient airflow. |
| One Size Everywhere | Mains and branches carry mismatched loads. | Nearby machines pull strongly while distant tools starve. | Size branches individually and step up the main. |
| Stepped Main | Area grows as active branch airflow joins. | Stable transport with less avoidable resistance. | Use gradual transitions and shallow-angle wyes. |
Simultaneous use changes the calculation.
A one-person shop may isolate machines with blast gates. A two-person shop may need the planer and table saw at once. The shared main must carry their combined demand, while the fan must still overcome pressure loss along every active route.
Let the air travel cleanly.
Every hood, elbow, reducer, gate, hose, separator, filter, silencer, and exhaust component consumes pressure. Short, smooth routes leave more of the fan’s capacity available for useful capture.
Rigid round duct
Smooth walls reduce friction and resist the internal ledges where debris can collect.
Long-radius elbows
Gentler turns reduce turbulence, wear, and the pressure penalty of abrupt direction changes.
Directional wyes
Shallow branch entries guide merged air in the direction of main-duct flow.
Flexible hose
Corrugations create major resistance. Use only short, straight lengths where movement is essential.
Abrupt transitions
Sharp reducers, square tees, and opposing streams create turbulence and unstable transport.
Dead legs and low spots
Unused pockets and sagging runs create natural collection points for chips and fine dust.
Design from hood to exhaust.
Calculate the most demanding active route rather than adding the resistance of every branch. Then confirm that the fan curve provides the required airflow at the total static pressure of that critical path.
Pickup Hood
Intercept dust where it forms.
Branch Duct
Preserve capture CFM and velocity.
Main Duct
Carry combined active airflow.
Separator
Remove chips with known resistance.
Filter and Fan
Evaluate loaded operating pressure.
Exhaust
Discharge or return air safely.
Measure the system you built.
A free-air CFM label describes a fan without real ductwork resistance. Test the finished installation with realistic filter loading, gate positions, and simultaneous machine operation.
Hardest route
Measure the pickup farthest from useful fan pressure.
Loaded filter
Test beyond the clean-filter best case.
Active branches
Confirm combined airflow under real use.
Baseline data
Record airflow and pressure after commissioning.
Deposits
Treat recurring buildup as a fault to investigate.
Get the Two Air Speeds Right Before You Choose Any Pipe
Maximizing Dust Collection Efficiency with Piping Layouts starts by separating capture airflow from conveying velocity. Capture airflow pulls debris into the hood before it escapes, while conveying velocity keeps that captured material moving through the pipe. You need both, because strong transport inside the duct cannot recover dust that the hood already missed.
The basic relationship is airflow Q = velocity V × duct area A. If you push the same CFM through a larger duct, the air slows down. If you squeeze it through a smaller duct, the air speeds up, but friction, noise, motor load, and pressure loss rise.
For instance, suppose a branch carries 400 CFM. In a 4-inch round duct, the average velocity is roughly 4,600 feet per minute; in a 6-inch duct, it falls near 2,000 feet per minute. The larger pipe looks generous, yet coarse planer chips may tumble, scrape, and collect along its bottom because the fan did not supply the added volume that larger area demands.
Woodworking guidance often references about 3,500–4,500 feet per minute as a broad transport range, but that is not a universal setting. Fine dry sanding dust behaves differently from damp planer curls, dense chips, or long fibrous shavings. According to the ACGIH Industrial Ventilation manual [2], hood capture and material transport require separate design decisions based on the process and contaminant.
The hood deserves equal attention. A table-saw cabinet with wide gaps may swallow hundreds of CFM while the blade throws a tan rooster tail above the table. Add a close-fitting overarm guard with a 2.5-inch or 3-inch pickup, and you catch dust where it forms instead of asking a distant cabinet port to bend airborne particles around the blade.
Good ductwork cannot rescue a poor pickup hood. Put the opening close to the dust stream, aim it with the direction of travel, and keep it out of the stock path.
Your first challenge is simple: watch the dust at each machine before drawing pipe lines. The hiss at a hood, the gray plume near a sanding belt, and the chips bouncing past a jointer chute tell you where capture fails first. Fix that point before buying another length of duct.
As an affiliate, we earn on qualifying purchases.
Choose a Duct Diameter That Preserves Both CFM and Velocity
Maximizing Dust Collection Efficiency with Piping Layouts requires sizing each section for the air volume it actually carries. A single-machine branch follows that pickup’s demand, while a main normally grows after branches merge. Copying the collector’s inlet diameter across the shop ignores velocity, simultaneous use, and resistance.
The table below shows the tradeoff you face. These are layout tendencies, not automatic prescriptions, because your fan curve, hood demand, material, filter condition, and operating pattern set the final dimensions.
| Layout choice | What happens | What you may notice | Better response |
|---|---|---|---|
| Duct too large | Velocity drops at the available CFM | Chips collect in horizontal runs and low spots | Match diameter to required airflow and transport speed |
| Duct too small | Friction and static-pressure loss rise | High-pitched hiss, weak distant pickups, heavy restriction | Use a larger section where combined airflow supports it |
| One diameter everywhere | Mains and branches carry mismatched loads | Nearby tools pull well while distant tools starve | Size branches individually and enlarge the main progressively |
| Properly stepped main | Area grows as branch airflow joins | Stable transport with lower avoidable resistance | Use gradual reducers and shallow-angle wyes |
Consider a small garage with a table saw, jointer, and thickness planer, where you run only one machine at a time. A 6-inch main with carefully sized drops may work well if each open branch supplies enough volume, but leaving three gates open can divide the airflow until none of the hoods performs properly. The collector did not become weaker; you changed its operating point.
A two-person shop creates a different problem. If the planer and table saw run together, the main beyond their junction must carry their combined demand. That does not mean adding every nameplate CFM and calling the result finished, because both active paths must also fit within the fan’s available pressure at that total volume.
Do not reduce a machine’s factory port merely because smaller hose is cheap or already on the wall. A 6-inch planer outlet necked to 4 inches can whistle sharply while chips pile inside the hood. Likewise, replacing every 4-inch branch with 6-inch pipe may slow transport if your collector cannot deliver the corresponding airflow.
Use the machine port as a clue, not a verdict. Calculate from pickup demand, target conveying speed, and realistic resistance, then compare that requirement with the fan curve. That approach protects both CFM and the speed needed to carry the material home.
As an affiliate, we earn on qualifying purchases.
Lay Out Shorter Runs That Stop Fittings From Stealing Airflow
Maximizing Dust Collection Efficiency with Piping Layouts gets easier when air travels through short, smooth, direct routes. Place the collector near high-demand tools, use rigid round duct for fixed runs, join branches with directional wyes, and reserve corrugated hose for brief machine connections that truly need movement.
A compact routing plan usually beats an elegant-looking maze. In one common garage layout, moving a planer five feet closer to the central main can remove ten feet of hose, two elbows, and a vertical climb. The motor sounds less strained, and the first board sends chips away with a crisp zip-whoosh instead of leaving curls in the chute.
- Place the demanding machines first. Start with the planer, jointer, drum sander, or CNC because these tools need high volume or produce debris continuously.
- Draw the critical branch. Give the farthest or most restrictive pickup the straightest practical route to the collector.
- Build a progressive main. Add branch airflow through shallow-angle wyes and enlarge the main where the combined volume calls for more area.
- Replace tight corners. Use long-radius elbows or two gentler bends when headroom permits.
- Trim flexible connections. Leave enough hose for vibration or adjustment, but remove slack loops that sag like a ribbed snake behind the machine.
- Add access points. Put cleanouts near long horizontal runs, low spots, branch ends, and bends that could trap damp or fibrous debris.
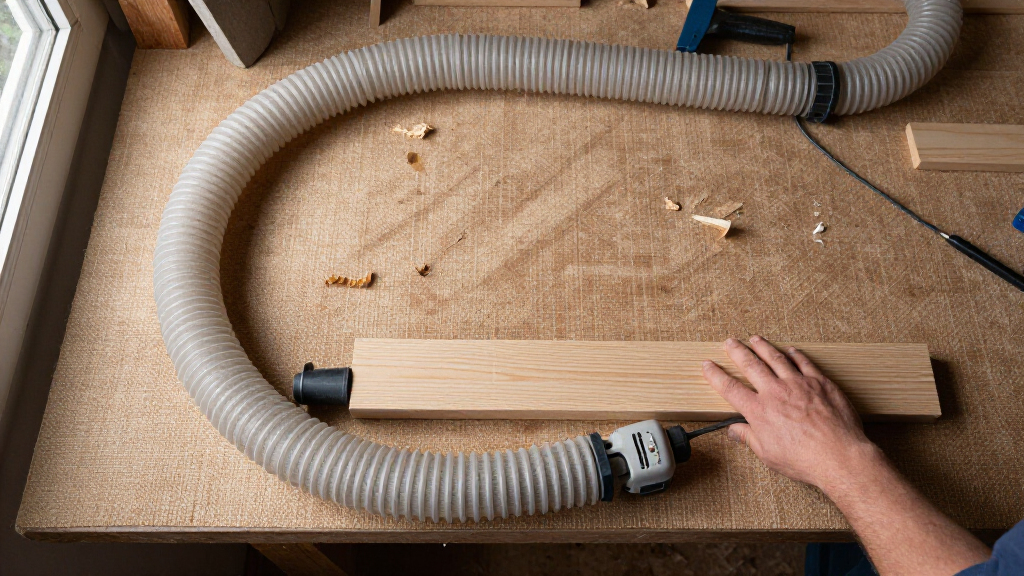
Corrugated hose is especially hungry for pressure. Its ridges churn the moving air, and a sag creates another pocket where chips can lose speed. Five feet at a mobile table saw may be a fair trade for movement; twenty-five feet hung across rafters usually is not.
Junction direction matters too. A square 90-degree tee makes the incoming stream crash into the main, producing turbulence, noise, and wear. A 30- or 45-degree wye lets the branch merge in the direction of travel, much like entering a road through a sloped ramp instead of driving straight through a barrier.
Keep elbows away from fan inlets and busy junctions when space allows. Air leaving a tight elbow swirls unevenly, and that distorted flow can hurt fan performance or make one branch rob another. A short straight section helps the stream settle before it meets the next fitting.
Support rigid pipe well enough that joints remain aligned and sealed. A long metal run that droops between straps develops leaky seams and low pockets, often marked by a faint brown crescent of chips. Your layout should stay smooth inside, so avoid protruding screws that can snag shavings and start a stubborn nest.
long radius elbows for dust collection
As an affiliate, we earn on qualifying purchases.
As an affiliate, we earn on qualifying purchases.
Find the Critical Path Before a CFM Rating Fools You
Maximizing Dust Collection Efficiency with Piping Layouts means testing the most demanding active route, not adding the resistance of every idle branch. Calculate the path from the hardest pickup through its duct, separator, dirty filter, fan, and exhaust, then confirm that the fan supplies the required CFM at that total static pressure.
The large number printed on a collector carton is often a free-air CFM rating. That measurement does not include your hood, thirty feet of pipe, cyclone, filter, gates, or four elbows. Once connected, the fan settles at the point where its performance curve meets the resistance of the real system.
Imagine a collector advertised near 1,200 CFM. Your farthest sander branch includes 35 feet of duct, three tight bends, a long hose, a separator, and a loaded cartridge filter. The sander may receive only a fraction of the advertised volume even while the bag snaps tight and the motor makes plenty of noise.
Pressure loss comes from every piece the air touches: pickup hoods, straight-duct friction, wyes, elbows, reducers, gates, cyclones, filters, silencers, and exhaust components. Dirty filters deserve special attention because their rising resistance shifts the fan toward a lower-airflow operating point. A design that barely works with a fresh white filter will disappoint once that filter turns tan and packed.
When two machines run at once, perform two checks. Confirm that the fan can supply their combined airflow, then calculate pressure along each active route. A short nearby branch can consume more than its share while a distant hood fades, so larger systems may need engineered balancing rather than partially closed gates chosen by ear.
A high-pressure shop vacuum and a high-volume dust collector also solve different problems. A vacuum handles a narrow tool port and long small hose well, while a dust collector moves more air through larger hoods and ducts. Connecting a shop vacuum to a 6-inch main is like trying to fill a sail with a bicycle pump: pressure is available, but the air volume is far too low.
Use published fan curves that show CFM against static pressure, not a single headline number. Include realistic filter loading and every component on the critical path. If the manufacturer supplies no useful curve, you have no reliable way to predict whether the fan and your proposed layout will meet at a workable point.
blast gate for dust collection system
As an affiliate, we earn on qualifying purchases.
As an affiliate, we earn on qualifying purchases.
Use Gates, Seals, and Controls Without Starving Distant Machines
Maximizing Dust Collection Efficiency with Piping Layouts depends on controlling where air enters without letting open gates, leaky joints, or automated fan settings cut transport speed. Gates should isolate inactive branches, seals should stop unwanted air, and controls should preserve capture volume plus minimum conveying velocity in every permitted operating setup.
Manual blast gates work well in a one-person shop when you use one major machine at a time. Put each gate near the branch takeoff or within safe reach, label it clearly, and develop a simple habit: open the working machine, close unused branches, then start the collector. A bright strip of tape on each handle makes a half-open gate easy to spot across a dim garage.
The tradeoff appears when your habits change. You may design around one open 6-inch branch, then leave a floor sweep and miter-saw gate open while planing boards. Air rushes through the easy openings, the planer branch loses volume, and thick curls begin collecting with a soft scritch-scritch inside the horizontal main.
Leaks create the same theft without announcing themselves. On a negative-pressure system, outside air gets pulled through loose clamp joints, access doors, gate slots, and collector connections, so you may never see a dusty plume. Seal suitable joints with products rated for the duct material, pressure, temperature, and dust service, then inspect them after vibration and seasonal movement.
Automated gates and variable-frequency drives can cut energy use in larger shops. Machine-status signals open the required damper, while the fan changes speed to match demand. The control logic still needs a floor: reducing speed too far can leave enough suction to look tidy at the hood while chips quietly fall out farther downstream.
Continuous pressure or airflow sensing gives you a clearer warning. A baseline reading at a planer hood lets you recognize a clogged filter, blocked branch, slipping fan drive, wrong gate position, or new leak before collection collapses. Filter differential-pressure monitoring also tells you more than cleaning cartridges on an arbitrary calendar.
A gate changes the entire network. Treat every allowed gate combination as an operating condition, especially when two people can start machines at the same time.
For a small shop, you do not need a wall of industrial controls. A handheld airflow instrument, a filter-pressure gauge, labeled gates, and recorded baseline readings can reveal most gradual problems. Spend first on sound piping and measurable airflow; add automation when it solves a real operating or energy problem.
Commission the System Safely and Catch Problems Before Dust Builds Up
Maximizing Dust Collection Efficiency with Piping Layouts ends with measured commissioning, regular inspection, and a safety review suited to the dust. Check airflow, duct velocity, static pressure, filter pressure drop, deposits, gate positions, noise, and vibration under the same machine combinations you expect to use.
Begin with clean filters and record the fan speed, motor current, filter pressure drop, and airflow at representative hoods. Repeat key readings after normal filter loading. Those numbers create a shop baseline, so six months later you can distinguish a dirty filter from a leaking branch or a machine hood clogged with planer curls.
Look inside accessible runs after the first week of use. A light film is different from a ridge of chips sitting along the bottom of a horizontal pipe. Repeated deposits point to low transport velocity, moisture, poor startup sequencing, an obstruction, or the wrong operating gate combination; cleaning alone only resets the symptom.
Wood dust also carries fire, explosion, and health hazards. According to NFPA 660, combustible-dust protection is addressed through a unified framework covering hazard analysis, prevention, and protection [1]. Bonding and grounding can reduce certain static-charge hazards, but they do not replace ignition control, housekeeping, explosion isolation, venting, suppression, or properly selected equipment.
A small home shop and an industrial plant do not share the same scale, yet neither gets a free pass on electrical or fire safety. Shut off and lock out power before working near fans, starters, or moving machinery, and wear eye protection, hearing protection, and a suitable respirator during dusty inspection or cleanup. Hire a licensed electrician for new circuits, motor controls, or VFD wiring, and follow permits, electrical codes, manufacturer instructions, and local fire rules.
Returning filtered air indoors needs careful review. Fine, sensitizing, toxic, or combustible dust can make recirculation unsuitable without suitable filtration, monitoring, and code approval. Industrial systems, indoor collectors, explosion controls, and structural duct supports should be designed or reviewed by qualified professionals and the authority having jurisdiction.
For instance, a cartridge may look clean from the outside while its pressure drop has doubled. Your pickup hood now whispers instead of snapping scraps against the grille, yet no visible duct leak appears. The gauge catches the restriction before a pale haze begins floating through a sunbeam beside the sander.
[1] NFPA 660, Standard for Combustible Dusts, provides the consolidated combustible-dust framework. [2] ACGIH Industrial Ventilation supplies established methods for hood design, airflow requirements, duct transport, and pressure-loss calculations. Apply the edition adopted by your jurisdiction and any stricter workplace or insurer rules.
Frequently Asked Questions
What diameter should I use for home-shop dust collection pipe?
Choose diameter from the airflow required at the hood and the velocity needed to carry your material. A machine port or collector inlet offers a starting clue, but neither accounts for branch length, fittings, filter resistance, or multiple open gates. Many garage systems use 4- to 6-inch branches, yet the right size comes from the complete airflow calculation.
Is bigger dust collection ductwork always better?
No. A larger duct lowers velocity when the fan does not supply more CFM, which can let chips settle in horizontal runs. A duct that is too small raises friction and pressure loss, so aim for a diameter that balances transport speed and resistance rather than choosing either extreme.
How much flexible hose can I use?
Use as little corrugated hose as practical, mainly where a machine moves, vibrates, or needs an adjustable connection. Keep it short, straight, and free of sagging loops. Replacing a long overhead hose with smooth rigid duct often produces a more useful airflow gain than buying a slightly larger collector.
Why is suction weak at the farthest machine?
The distant branch may combine too much duct length, tight elbows, undersized pipe, flexible hose, leakage, dirty filters, or competition from open gates. Check the complete route and compare hood airflow with your commissioning baseline. If the branch has always been weak, compare its calculated resistance with the fan curve rather than adjusting gates by sound alone.
Are 45-degree wyes better than 90-degree tees?
Yes, in most dust collection layouts. A directional wye guides branch air into the main with less turbulence, impact, and pressure loss than a square tee. It also gives chips a smoother path, reducing the chance that debris will collect at the junction.
Can one dust collector serve several machines?
Yes, when the fan, filter, separator, ductwork, and controls support the machines that may run together. A layout designed for one open branch can lose capture and transport speed when two or three gates open. Calculate combined airflow and verify pressure along every active path you plan to permit.
Does grounding prevent a wood-dust explosion?
No. Bonding and grounding address certain electrostatic ignition risks, but they do not stop sparks, hot particles, friction, or every other ignition source. Combustible-dust protection may also require hazard analysis, suitable electrical equipment, isolation, venting, suppression, housekeeping, and review by qualified professionals under NFPA 660 and local rules.
Conclusion
Your most useful move is to trace one complete route from the cutter to the exhaust and remove every avoidable restriction along it. Match the hood, branch diameter, fittings, fan curve, separator, and loaded filter as one system, then prove the result with airflow and pressure readings. A larger fan cannot erase poor geometry, and a larger pipe cannot create CFM the fan does not deliver.
Start with your dustiest machine this weekend. Shorten the ribbed hose, replace the square tee, seal the loose joints, and mark a baseline reading at the hood. When the next board passes through and the chips vanish with a sharp thump-whoosh instead of hanging in the warm shop light, you will hear what an efficient layout sounds like.
Fall Picks
fall essentials
As an affiliate, we earn on qualifying purchases.